
What works in the lab must make sense in the mill
Why successful textile finishing scale-up depends on transferring knowledge, not simply...
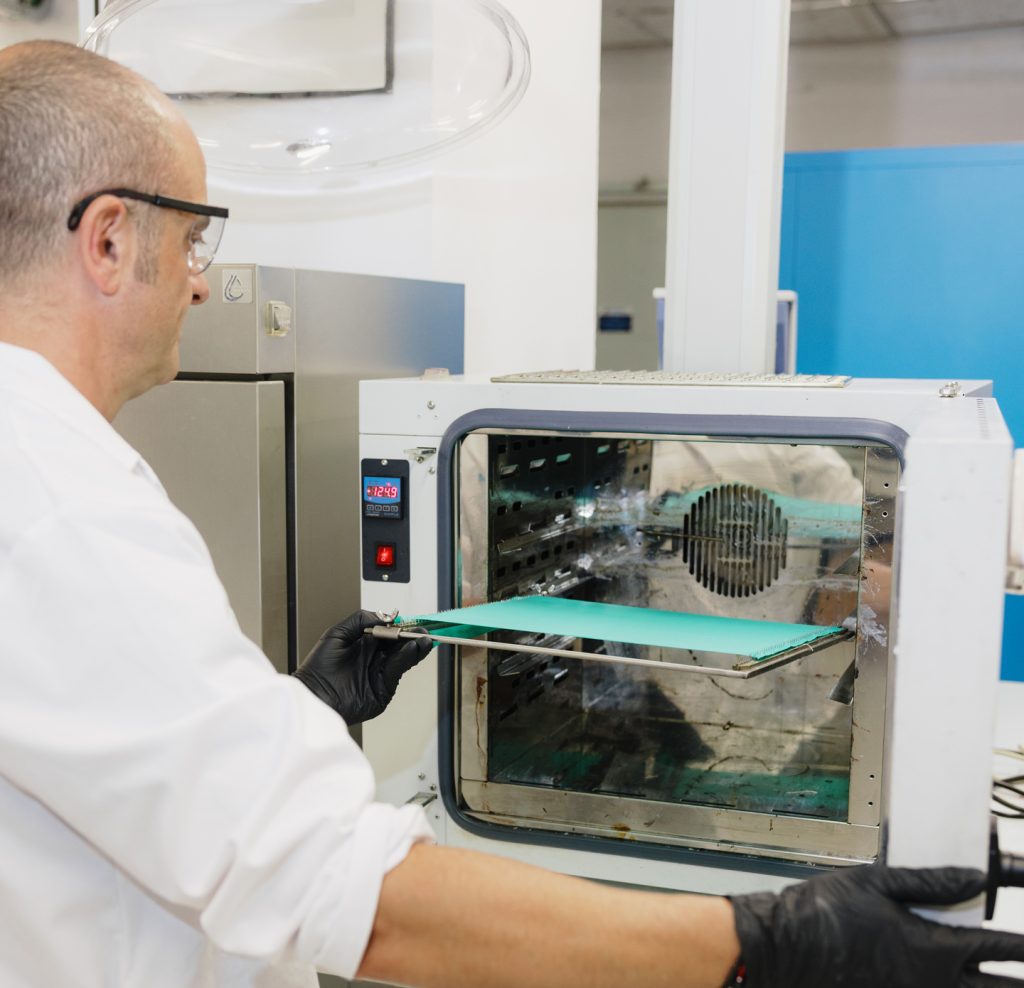
Why successful textile finishing scale-up depends on transferring knowledge, not simply reproducing a recipe.
A successful laboratory trial gives us something valuable: evidence that a formulation can deliver the expected result under a defined set of conditions.
The next step may seem straightforward. If the formulation works at laboratory scale, we reproduce the recipe at a larger volume and move towards industrial production.
But scale-up is not simply a question of increasing quantities.
A textile finishing recipe describes products, concentrations and application parameters. The result, however, depends on the relationships between chemistry, substrate, equipment and process conditions. When the scale changes, some of those relationships change with it. Heat and mass transfer, application dynamics, contact times or the behaviour of the substrate cannot necessarily be reproduced by multiplying the numbers in a laboratory recipe.
This is why the real challenge is not to make the laboratory bigger. It is to understand what made the laboratory result possible and determine how those conditions can be translated into an industrial environment.
Pilot-scale facilities exist partly to bridge this gap: to move from controlled experimentation towards conditions that are representative of industrial production, while still allowing the process to be observed, adjusted and understood. CETI and RISE are examples of textile research organisations using pilot-scale environments to support this transition from development to industrial implementation.
Scale-up is translation, not multiplication.
And what needs to be translated is not only the formulation. It is the knowledge behind the result.
A lab result tells us that something works
The laboratory gives us something industrial production rarely can: a controlled environment in which variables can be isolated, formulations compared and performance evaluated under repeatable conditions.
This makes laboratory testing essential. It allows us to determine whether a finishing concept is technically viable, compare different formulations and observe how changes in chemistry or application conditions affect the textile.
But a successful result tells us more than what is written in the recipe.
Behind that result is a particular combination of substrate characteristics, product concentration, application method, wet pick-up, temperature, time and other process conditions. These variables do not simply coexist: they interact. Change one of them and the relevance of another may change too.
This distinction matters when we move towards industrial production. If we transfer only the formulation — products, concentrations and nominal parameters — we may be transferring the instructions without transferring enough of the knowledge that made them work.
The purpose of laboratory development, therefore, is not only to find a combination that produces the desired performance, but also to begin understanding why that combination works and which conditions are critical to maintaining the result.
This changes the question we ask before scale-up.
Not simply:
What recipe should we reproduce?
But:
What, exactly, needs to be transferred for this result to remain meaningful at industrial scale?
You scale relationships, not recipes
A laboratory recipe can be expressed in numbers: product concentration, liquor ratio, temperature, time or application level. Those numbers are necessary, but reproducing them does not necessarily reproduce the process.
In textile finishing, performance often depends on the relationship between variables.
Take a conventional padding process. The amount of finishing chemistry deposited on the fabric is not determined by bath concentration alone. It also depends on wet pick-up, which in turn is influenced by fabric characteristics, machine settings and the properties of the finishing liquor. Consistent application requires factors such as nip pressure, bath level, temperature and fabric speed to remain sufficiently controlled.
The same principle continues downstream. After padding, drying removes water and curing enables the reactions or fixation required by many finishes. Temperature cannot therefore be considered independently from residence time, just as concentration cannot be considered independently from the amount of liquor actually retained by the textile. The standard pad-dry-cure sequence is itself a chain of interdependent stages, each capable of influencing the final result.
This is why scale-up becomes less about preserving individual numbers and more about understanding how the relevant variables influence one another. The relationship between chemistry and substrate matters; concentration only makes sense alongside the amount of liquor retained by the fabric; temperature has to be considered together with exposure time; and the way a finish is applied affects how it is subsequently fixed.
At industrial scale, equipment geometry, line speed, fabric construction or application technology may be different from the conditions used during development. The objective is therefore not necessarily to make every parameter identical. It is to understand which relationships produced the desired effect and how they can be maintained under a different set of physical conditions.
A recipe can be multiplied. A process cannot.
And that distinction changes the purpose of scale-up: we are not simply transferring quantities from one vessel or machine to another. We are transferring an understanding of the process that must continue to produce the intended textile performance.
Equivalent does not mean identical
Moving from the laboratory to industrial production does not mean recreating laboratory conditions on a larger machine. In many cases, that would not even be possible.
Industrial equipment has its own geometry, operating speeds, heating and drying capacity, application systems and control mechanisms. The amount of material being processed changes, but so does the way energy and chemicals are transferred through the system. This is one of the reasons why scale-up is generally approached through equivalent process conditions rather than simple geometric enlargement.
For textile finishing, the distinction is particularly relevant. A laboratory padder and an industrial padding line may perform the same basic operation, for example, but differences in nip configuration, pressure, speed or fabric behaviour can affect liquor retention and ultimately the amount of chemistry applied. Likewise, reproducing a curing temperature does not necessarily reproduce the same thermal history if heating rates and residence times are different.
The aim, therefore, is not to ask whether the mill can reproduce every laboratory parameter exactly. It is to identify which conditions are critical to the intended performance and determine how they can be achieved with industrial equipment.
This is where pilot-scale testing becomes particularly valuable. Pilot environments provide an intermediate step between controlled laboratory development and full production, allowing formulations and processes to be tested with equipment and operating conditions that are closer to industrial reality. Research and technology organisations use these facilities not simply to repeat laboratory trials at a larger size, but to evaluate how a process behaves as it moves towards industrial implementation.
In other words, successful transfer does not depend on making the mill behave exactly like the lab. It depends on understanding the laboratory result well enough to know what needs to remain equivalent when everything around it changes.
Good transferability also means knowing what can change
If successful scale-up required every parameter to remain fixed, very few laboratory processes would survive the transition to industrial production.
Variation is part of manufacturing. Raw materials and textile substrates can differ between batches, equipment operates within tolerances, and environmental or process conditions are never perfectly static. The objective is therefore not to eliminate every source of variation, but to understand which changes matter to the result and which ones the process can accommodate.
This requires a different kind of knowledge from simply identifying the conditions that produced the best laboratory sample. Development also needs to reveal how sensitive the result is when those conditions move. A small change in one parameter may have little practical effect, while a similar change elsewhere may alter repellency, handle, colour, adhesion or another critical property.
This is closely related to the principles of Quality by Design, where process understanding comes not only from defining a target condition, but from understanding the relationship between material attributes, process parameters and product performance. The framework comes from pharmaceutical development, but the underlying engineering principle is useful here: knowing how a process responds to variation provides more information than knowing its optimum setting alone.
For textile finishing, this does not mean accepting inconsistency. It means distinguishing between variation that is operationally manageable and variation that changes the performance we are trying to preserve.
That distinction makes transferability more practical. Instead of taking a laboratory recipe to the mill with the expectation that production will reproduce an ideal set of conditions, we take something more valuable: an understanding of what must be protected, what can be adjusted and where a change begins to matter.
A transferable process, in other words, is not one that depends on everything remaining exactly the same. It is one that has been understood well enough to work when reality is not.
The mill does not simply validate R&D
It is tempting to think of industrial production as the final checkpoint in the development process: the formulation has been designed in the laboratory, refined through trials and is now taken to the mill to confirm that it works.
But industrial implementation can do more than validate what R&D already knows. It can generate new knowledge.
At production scale, a formulation encounters conditions that are difficult to reproduce completely in the laboratory or even at pilot scale. Longer production runs, changes between fabric lots, equipment behaviour, operating rhythms and the interaction between consecutive stages can reveal effects that were not significant — or simply not visible — during development.
These observations are valuable because they can expose assumptions made earlier in the process. A parameter considered secondary in the laboratory may become important at production scale. An adjustment made to accommodate industrial equipment may reveal a more efficient way of applying the finish. A difference between batches may help identify a substrate characteristic that deserves closer attention.
This is why technology transfer should not be understood as a one-way handover from R&D to production. Industrial transfer can create a feedback loop in which what is learned during implementation returns to development and helps refine the formulation, the application method or the way future trials are designed.
The relationship between laboratory, pilot and mill is therefore less linear than it first appears. Each stage answers different questions, and each can change what we need to investigate at the others.
The mill is not simply where R&D proves that it was right. It is another place where the process is understood better.
Conclusion
Scale-up often begins with a practical question: can we reproduce this laboratory result at industrial scale?
It is a necessary question, but perhaps not the most useful one.
As we move from laboratory development to pilot trials and industrial production, the objective is not simply to preserve a formulation. It is to preserve the understanding behind its performance: which relationships matter, which conditions need to remain equivalent, which parameters can change and how the process responds when they do.
That understanding is what makes adaptation possible. It allows a formulation to move between different equipment, substrates and production conditions without treating every change as a departure from the original laboratory result. And when industrial implementation reveals something unexpected, that information can become part of the development process rather than simply being classified as a production problem.
So instead of asking only:
Can we reproduce this laboratory recipe at industrial scale?
A more useful question may be:
Do we understand the result well enough to reproduce its performance within the realities of industrial production?
The distinction matters. A successful laboratory trial demonstrates that a result is possible. Successful transfer demonstrates that we understand enough about that result to make it relevant beyond the conditions in which it was first achieved.
What works in the lab must do more than work again at scale. It must make sense in the mill.